 EN EN
Directly sourced from our vertically integrated mineral processing facilities and automated OEM bag converting lines.
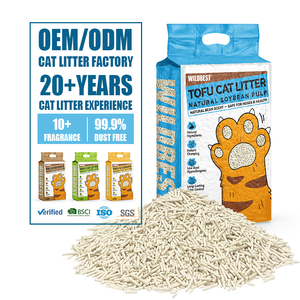
The global pet hygiene sector has experienced a profound shift over the last decade. As cat ownership surges worldwide, cat litter packaging is no longer viewed merely as a container; it has evolved into a high-engineered barrier shield critical to product integrity, brand prestige, retail logistics, and consumer satisfaction. Sourcing cat litter bags from a premier China factory requires a comprehensive understanding of polymer material science, tensile strength dynamics, moisture-vapor barrier performance, micro-perforation venting, and retail ergonomics.
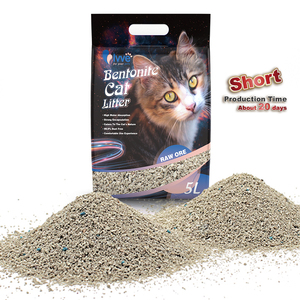
Cat litter substrates—ranging from dense sodium bentonite clay (bulk density ~0.9 to 1.1 g/cm³) to lightweight plant-based tofu, wood, and silica gels—present distinct mechanical and chemical packaging challenges. Dense sodium bentonite exerts intense static hydrostatic pressure against bag seams during shipping and pallet stacking. Without multi-layer co-extrusion technology, localized strain points often lead to catastrophic seam bursts, flex-cracking, and product leakage during maritime transport.
Key Engineering Insight: High-performance heavy-duty cat litter bags must balance structural tensile strength with flexural crack resistance. Utilizing high-density polyethylene (HDPE) combined with metallocene linear low-density polyethylene (mLLDPE) provides superior puncture resistance against abrasive mineral edges while retaining high drop-impact absorption up to 2.5 meters.
When engineering 5kg, 10kg, 15kg, and 20kg cat litter bags for international export, factories must address four critical physical failure modes:
Choosing the correct flexible packaging material structure determines shelf life, durability, and brand presentation. The comparison matrix below outlines the leading engineered film structures manufactured in our state-of-the-art Chinese facility:
| Material Structure | Barrier Class | WVTR (g/m²/24h) | Tensile Strength | Best Application | Sustainability Profile |
|---|---|---|---|---|---|
| PET / NY / mLLDPE | High Barrier | < 1.2 | Ultra-High (> 55 MPa) | 10kg - 20kg Heavy-Duty Bentonite Bags | Standard Recyclable Stream |
| PET / VMPET / PE | Extreme Barrier | < 0.5 | High (> 42 MPa) | Premium Scented & Silica Gel Litters | Multi-layer Mixed Film |
| Kraft Paper / VMPET / PE | Organic / Barrier | < 1.0 | Medium-High | Eco Tofu & Natural Wood/Pine Litter | Partial Bio-content Look |
| Mono-Material HDPE/LLDPE | Eco-Engineered | < 2.0 | High-Toughened | 5kg - 10kg Universal Eco-Litters | 100% Fully Recyclable (RIC 4) |
| Woven PP / PE Lamination | Bulk Commercial | < 3.5 | Extreme Tensile | 15kg - 25kg Economy & Institutional Bags | Heavy-Duty Reusable / Industrial |
For premium retail brands, our Quad Seal Box Pouches (Flat Bottom Bags) offer five distinct printable panels, maximizing shelf presence while maintaining structural rigidity. Integrated ergonomic carry handles—such as die-cut reinforced handles, plastic soft-loop handles, or top-applied heavy-duty G-handles—are stress-tested to endure over 250 N of pulling force without plastic deformation or tear propagation.
Unlike standard trading intermediaries or localized bag converters, our organization operates under a fully integrated vertical manufacturing model. Building upon over 35 years of deep expertise across raw mineral extraction and polymer converting, we deliver unparalleled supply chain security and consistency to international buyers.
We control the complete value chain from raw sodium/calcium bentonite mineral extraction and rheological processing to high-definition flexographic film printing, lamination, and automated bag conversion.
Every production batch passes strict drop-impact testing (ASTM D5276), seal strength testing (ASTM F88), burst pressure evaluation, and 10-color HD gravure/flexographic print alignment checks before release.
Trusted by major supermarket chains, wholesalers, and specialist pet distributors across 50+ countries. Committed to social responsibility, having donated over 150,000 liters of hygienic cat litter to animal shelters.
This holistic operational framework guarantees that when global pet brands source both cat litter formulations (bentonite, tofu, silica) and custom private-label cat litter bags from our factory, they benefit from synchronized lead times, consolidated freight logistics, and reduced total cost of ownership (TCO).
Driven by strict environmental legislation such as the European Union’s Packaging and Packaging Waste Regulation (PPWR) and shifting consumer expectations, the pet packaging landscape is undergoing rapid technological innovation. Forward-thinking procurement teams must prepare for three major structural shifts:
Traditional multi-material laminates combining PET, Foil, and PE are difficult to recycle due to layer separation constraints. Modern advanced polymer chemistry enables Mono-PE flexible laminates (Oriented PE / PE + metallocene sealing layer). These structures match the tensile strength and burst resistance of PET/PE laminates while qualifying for single-stream PE recycling loops (Store Drop-off / RIC 4), allowing brands to display eco-certified logos on shelf.
To reduce virgin fossil fuel reliance, leading brands are mandating 30% to 50% PCR content in heavy-duty outer films. Through multi-layer co-extrusion technology, PCR materials are encapsulated within inner structural layers, preventing any contact with internal pet care products while retaining pristine exterior printability and visual clarity.
Dense cat litter packing lines generate significant residual air during high-speed automated filling. Trapped air inflates bags, reducing pallet density and risking bag rupture during high-altitude transit or stacking. Our factory integrates micro-perforation matrix valves and selective one-way degassing valves that vent internal air without allowing exterior moisture ingress.
When selecting a Chinese cat litter bag manufacturer, professional sourcing directors should evaluate prospective factories across five core capability benchmarks:
Designed to provide instant clarity on common procurement inquiries from global pet care brands, distributors, and supply chain managers.
From initial design concept to international sea freight delivery, our factory adheres to a streamlined 6-stage production framework ensuring zero-defect execution:
We evaluate your litter density, target weight (5kg-20kg), drop test goals, and retail environment to select the optimal barrier film structure.
Our prepress team optimizes graphic artwork, executing up to 10-color gravure or high-definition flexo plate engraving for crisp photographic printing.
High-speed extrusion line combines resin polymers, followed by solvent-free lamination to eliminate volatile organic compounds (VOCs) and chemical odors.
Automated bag-making machinery forms side gussets, applies PTC zippers, punches micro-vent valves, and attaches heavy-duty carry handles.
Batch samples undergo seal burst testing, tensile elongation checks, 2.5m drop testing, and bar-code scannability validation.
Bags are shrink-wrapped on export pallets with moisture-proof covers, ready for direct container loading and ocean freight shipping.
Elevate your brand with industrial-grade heavy-duty bags, innovative eco-friendly flexible packaging, and full-chain OEM/ODM manufacturing excellence. Contact our engineering team today for factory-direct pricing, custom material samples, and technical specifications.
Inquire Now