 EN EN
High-margin OEM/ODM solutions tailored for global distributors, private label supermarket chains, and wholesale importers.
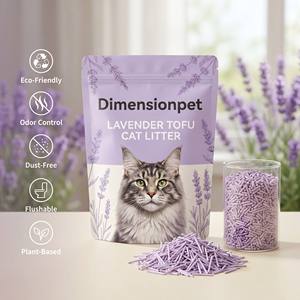
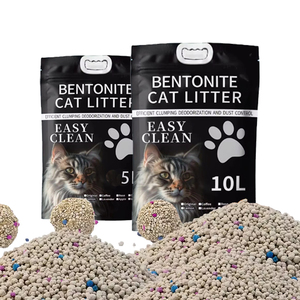
The global pet hygiene sector is undergoing a profound structural evolution. Driven by rapid urbanization, humanization of household pets, and stringent environmental regulations across North America and the European Union, procuring commercial cat litter has transitioned from a basic commodity transaction to a complex strategic decision. For professional procurement directors, brand owners, and retail chain buyers, selecting a verified CE Certified commercial cat litter manufacturer is paramount to risk mitigation, consumer safety, and multi-market commercial scaling.
Compliance with CE certification standards ensures that manufactured mineral-based, bio-based, and synthetic cat litters satisfy stringent safety directives regarding hazardous substance emission, respirable crystalline silica (RCS) safety limits, heavy metal non-toxicity (EN 71-3 standard benchmarks), and environmental chemical stability. As regulatory agencies intensify audit controls on imported pet products, partnering with an established manufacturer possessing complete vertical integration—from raw mineral extraction to automated high-speed packaging—offers unmatched supply chain resilience.
Uniquely positioned with over 35 years of industrial pet hygiene expertise, our manufacturing matrix overcomes the structural vulnerabilities common to third-party contract repackagers. By controlling the entire supply chain from raw mineral extraction through advanced bio-engineering synthesis to final private-label retail packaging, we deliver guaranteed batch stability and significant margin advantages for our commercial partners.
Proprietary access to high-purity Sodium Bentonite and Sepiolite deposits ensures superior cation-exchange capacity and natural high-expansion clumping capability without reliance on chemical binders.
State-of-the-art negative pressure cyclone dedusting chambers remove ultra-fine airborne dust down to sub-micron levels, yielding a 99.9% dust-free product suitable for sensitive cats.
Patented odor-lock technologies encapsulate liquid and volatile organic compounds (VOCs) instantly, locking away ammonia molecules (NH3) for extended multi-cat box fresh life.
Our manufacturing facility operates multiple high-capacity automated production lines capable of producing over 150,000 metric tons annually. Whether your strategy requires bulk super-sack shipments for regional packaging facilities or ready-to-shelf private-label retail pouching (ranging from 2.5kg vacuum-sealed tofu bricks to 20kg heavy-duty woven bags), our infrastructure scales seamlessly to accommodate your procurement roadmap.
To assist procurement teams in matching product specifications with consumer market demand, the following technical matrix outlines the chemical, physical, and functional characteristics of our core commercial cat litter formulations:
| Litter Category | Primary Composition | Absorption Rate | Clumping Speed | Target Retail Channel |
|---|---|---|---|---|
| Premium Sodium Bentonite | Natural Volcanic Sodium Bentonite Granules | > 350% by weight | < 3 Seconds (Solid) | Mass Retail, Supermarkets, Specialist Pet Chains |
| Plant-Based Tofu Litter | Pea Fiber, Food-Grade Starch, Guar Gum | > 400% by weight | < 5 Seconds (Flushable) | Eco-Specialist, E-Commerce Direct-to-Consumer |
| Lightweight Mineral Clumping | Expanded Sepiolite & Porous Clay Complex | > 300% by weight | < 4 Seconds (Lightweight) | Urban Retail, Convenience Stores, Senior Care |
| Absorbent Non-Clumping | High-Purity Natural Attapulgite / Mineral Clay | > 180% liquid lock | N/A (Liquid Retention) | Value Discount Chains, Commercial Shelters |
1. Hydration & Clumping Mechanics: Our engineered Bentonite litter utilizes specialized particle size grading (0.5mm - 2.5mm). When liquid contacts the granules, the sodium ions facilitate instant moisture expansion, creating dense, spherical clumps that resist crumbling during scooping. This minimizes litter wastage by up to 25% compared to standard commercial clays.
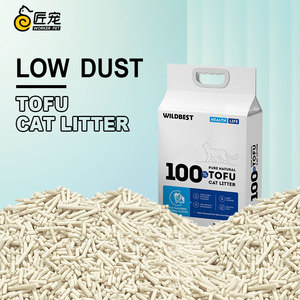
2. Bio-degradable Tofu Engineering: Formulated using upcycled food-grade pea fibers, our Tofu litter features a fast-dissolving micro-structure. When submerged in large volumes of water, the organic binders break down completely within 60 seconds, allowing safe municipal flushing while offering superior anti-tracking, dust-free performance in modern households.
As global market dynamics shift toward sustainability, carbon footprint reductions, and heightened product performance, commercial purchasing managers must anticipate category trends to maintain competitive advantage. Our R&D division has identified four megatrends shaping the cat litter industry over the coming decade:
Traditional heavy clay litters impose severe freight and logistics costs. Commercial buyers are aggressively shifting toward lightweight mineral formulations. By utilizing naturally porous minerals like Sepiolite, we reduce product weight by up to 40% without compromising volume or absorption capacity. This translates directly into lower transportation costs per container unit, reduced carbon emissions during maritime transit, and improved ergonomics for retail consumers.
Environmental regulations and eco-conscious shoppers are accelerating the growth of plant-derived litters. Using agricultural co-products—such as pea fiber, cassava starch, and wood pulp—creates a fully renewable product ecosystem. Future-proof brands are expanding their portfolios to include 100% biodegradable and compostable options to capture high-margin eco-driven market segments.
The integration of diagnostic capabilities into cat litter represents a breakthrough market innovation. By embedding safe, non-toxic pH-sensitive micro-indicators into the litter substrate, the sand changes color in response to abnormal urine pH levels or the presence of occult blood. This provides early detection of feline lower urinary tract diseases (FLUTD), creating an exceptionally sticky value-added retail product.
With the rapid growth of pet care e-commerce, transit volume optimization is vital. Vacuum-sealed "brick" packaging for tofu and mineral litters eliminates dead air space within master cartons, increasing container loading density by 35%. This innovation significantly reduces parcel delivery damages and optimizes warehouse storage efficiency.
We empower global brands to build distinct market identities through comprehensive OEM/ODM customization options. From custom scent formulation to tailored granule colors and bespoke packaging design, our turn-key manufacturing solution ensures rapid time-to-market.
Our global supply network guarantees transparent lead times, strict shipping schedules, and dedicated account management. Every commercial shipment is accompanied by a Certificate of Analysis (CoA), SDS documentation, and CE compliance proof to streamline customs clearance worldwide.
Detailed technical and operational answers to common inquiries from commercial buyers, distributors, and private label managers.
Sustainable manufacturing is no longer optional—it is a core pillar of our corporate philosophy. We are dedicated to reducing the environmental footprint of pet ownership through circular resource utilization, eco-friendly product lines, and active community outreach.
Our manufacturing plants utilize solar-assisted drying systems and closed-loop water recycling networks, minimizing industrial energy consumption. Furthermore, we actively support animal welfare organizations worldwide. To date, we have donated over 150,000 liters of high-grade cat litter to non-profit animal shelters, rescue groups, and feline adoption centers, ensuring clean and hygienic living conditions for vulnerable animals waiting for forever homes.